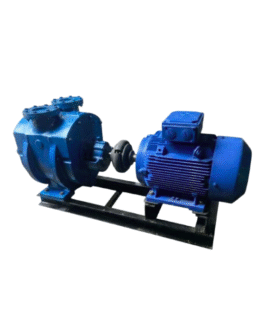
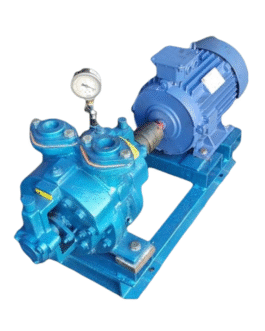
liquid ring vacuum pump

liquid ring vacuum pumps – Best price 2026

Achieve perfect vacuum levels with our versatile liquid ring vacuum pump. Built for robustness, it boasts capacities from 50 to 10,000 m³/hr. Order now!

  • Power Range: 3 HP to 75 HP
  • Vacuum Capacity: Up to 700 mm/Hg
  • Material Options: Cast Iron / SS 304 / SS 316
  • Suction Capacity: 50 m³/hr to 1800 m³/hr
  • Cooling Method: Water-cooled
  • Seal Type: Mechanical Seal / Gland Packing
  • Operating Speed: 1440 RPM

Fast & Reliable service

From Vacuum Pumps to Roots Blowers—One Reliable Partner

Description

Liquid Ring Vacuum Pump – Single & Two-Stage

ParameterSingle-Stage PumpTwo-Stage Pump
Vacuum LevelUp to 720 mmHgUp to 740 mmHg
Capacity Range50 to 10,000 m³/hr100 to 8,000 m³/hr
Power ConsumptionModerateOptimized for high vacuum
Sealing LiquidWater / Oil / SolventWater / Oil / Solvent
Temperature HandlingUp to 80°C (standard)Higher tolerance available
Material of ConstructionCI / SS / BronzeCI / SS / Alloy Steel
MountingBase Mounted / MonoblockBase Mounted

A Liquid (Water) Ring Vacuum Pump is a highly reliable and efficient device used to create vacuum in various industrial applications. It operates using a rotating impeller and a sealing liquid (usually water) to form a liquid ring that compresses and evacuates gases.

These pumps are widely preferred for handling wet, humid, and contaminated gases due to their robust and simple design.

Working Principle

Both single and two-stage pumps work on the same principle:

  1. An impeller rotates inside a casing partially filled with liquid.
  2. The liquid forms a ring due to centrifugal force.
  3. Gas enters through the inlet and gets trapped between impeller blades.
  4. The gas is compressed and discharged through the outlet.

In two-stage pumps, this process happens in two steps, allowing deeper vacuum levels.

Advantages of Liquid Ring Vacuum Pumps

  1. Can handle wet and corrosive gases
  2. Low noise and vibration
  3. No metal-to-metal contact (longer life)
  4. Easy maintenance
  5. Suitable for continuous operation

Accessories & Optional Features

Enhance the performance and lifespan of your vacuum system with the following accessories:

  1. Vacuum gauges
  2. Non-return valves
  3. Gas-liquid separators
  4. Heat exchangers
  5. Control panels (automatic / PLC-based)
  6. Silencers for noise reduction
  7. Mechanical seals / gland packing options

Why Choose Our Liquid Ring Vacuum Pumps?

  1. High efficiency and reliable performance
  2. Designed as per international quality standards
  3. Custom-built solutions available
  4. Competitive pricing
  5. Strong after-sales support
  6. Fast delivery across India and global markets
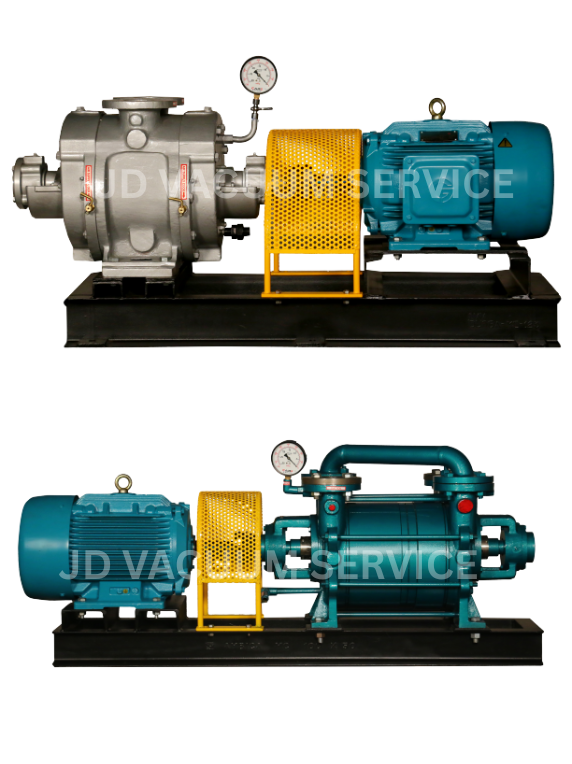
Liquid ring vacuum pump – JD VACUUM SERVICE

Type JDWVSpeed rpmsuction capacityRecommended
motor hp
Water consumption
ltr/min.
128505037
2285080510
328501207.514
414401607.515
514402201020
614403301530
714404402040
89807203060
99808453580
10980108040100
11725150065150
12725202590200

Material Of Construction:

  • Type: A (C.I. Construction)
  • Type: C (All Internal Parts in SS 304 / SS 316)
  • Type: SS (Complete SS 304 / SS 316)

Features

  • Simple Construction
  • High Capacity
  • Trouble-Free Operation
  • Low Maintenance

Applications

  • Chemical Industries
  • Pharmaceuticals
  • Sterilizing
  • Distillation, Evaporation & drying
  • Filtration Processes
  • Dehydrates
  • Conveying Sucking
  • Priming
  • Bottle Filling

Salient Features

  • Trouble-free Installation
  • Corrosion Free
  • Compact Model
  • Robust Construction
  • Portable
  • Excellent resistance capacity to extreme temperatures
  • Noise-free operation
  • Environment Friendly
  • Longer operational life
  • Highly durable